
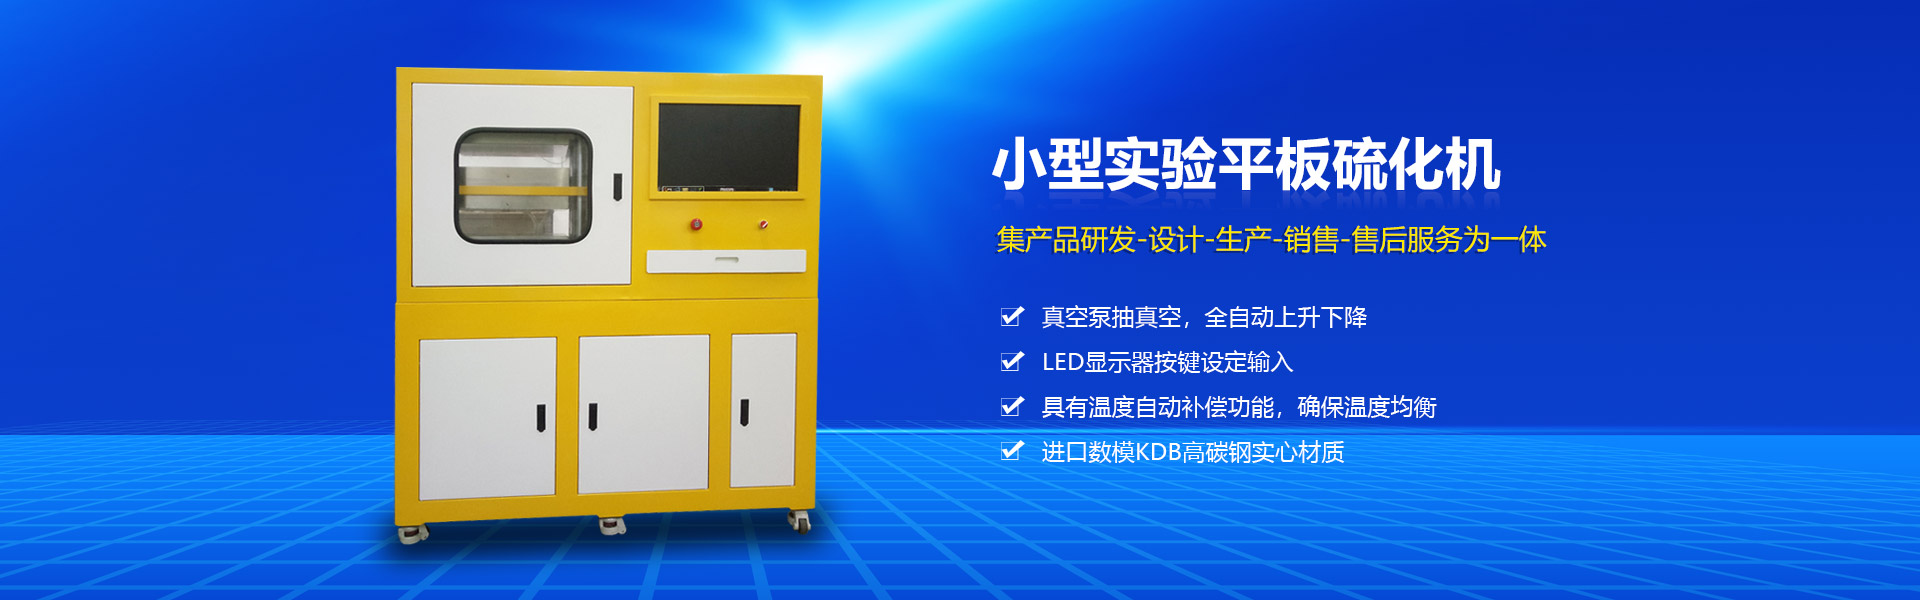

Main components and structure of the flat vulcanizing machine
To control the operation of a flat vulcanizing machine, several distribution devices are required. During the working stroke and vulcanization of the flat vulcanizing machine, the distribution devices connect the hydraulic cylinder and the high-pressure inlet pipe. When it is time to open the vulcanizing machine, the distribution devices connect the hydraulic cylinder to the drain pipeline. This type of distribution device for controlling the flat vulcanizing machine is called a distributor. Distributors come in several types, including sliding valve, plug valve, and gate valve.
A simpler slider valve distributor. The valve body features a cylindrical bore. Inside the bore, there is a slider 3 equipped with two rings 4, which are precisely fitted with the valve body's cavity. The slider can move left under the spring's influence or right under the force produced by solenoid 1. The valve body has channels (drilled holes) that connect to the working chamber of the flat die hydraulic cylinder via channel 5 and plate. High-pressure fluid enters through channel 7 and is connected to the return tank via channel 8. It can be observed that the slider's rings interrupt the fluid circuit. The high-pressure liquid conduit is connected to the pipe leading to the working cylinder chamber. The flat die press is in a pressure holding state.
When the electromagnetic coil is de-energized, the spring pushes the valve rod to the left. As the circular ring moves, it opens a hole connected to the liquid discharge pipeline. At this point, the two circular rings seal the high-pressure liquid input pipeline. Consequently, the liquid inside the hydraulic cylinder flows out, and the flat vulcanizing machine opens.
In industrial flat vulcanizing machines, more complex and sophisticated sliding valve distributors are typically used. However, these distributors also have significant drawbacks that limit their application. In such distributors, the sliding valve should fit very precisely with the inner surface of the valve body. Even slight defects or wear on the inner surface of the sliding valve can lead to a loss of sealing, rendering the distributor inoperable. Sliding valve distributors are only suitable for flat vulcanizing machines that use oil as the working fluid.
The disadvantages of the plug-valve distributors are their difficulty in achieving mechanized operation and slow switching processes. These distributors are typically installed on small or manually operated equipment.
Valve distributors are widely used in the control systems of vulcanizing machines. These distributors can be operated manually or controlled by cylinders and electromagnetic coils.
On the sulfur vulcanizing machines, which have many hydraulic components and complex monthly structures, each liquid input and output pipeline is equipped with an electromagnetic control valve or a pneumatic control valve, all controlled by a unified control instrument to ensure the valves are started in the required sequence.
To prevent shock when the valve core closes, a conical tube is typically used beneath the valve core. As the valve core approaches the seat, the conical tube gradually reduces the cross-sectional area of the seat, allowing the fluid flow to be cut off smoothly and slowly.